- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Concrete and Masonry
- Demolition & Excavation
- Electrical & Mechanical
- Fasteners and Anchoring Adhesives
- Floor Protection
- Generators and Welders
- Hand Tools
- Heaters
- Janitorial and Office Supplies
- Jobsite Protection
- Ladders & Storage
- Lighting & Lighting Accessories
- Man Lifts
- Material Handling Equipment
- Power Tools
- Pressure Washers & Pumps
- Safety Gear
- Safety Products
- Saws
- Surface Preparation
- SEASONAL PRODUCTS
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rentals
- Demolition & Excavation Equipment Rentals
- Concrete Floor Grinder Rentals
- General Construction Equipment Rentals
- Generator Rentals and Welder Rentals
- Heater Rentals
- Light Tower Rentals
- Man Lift Rentals in Massachusetts and Rhode Island
- Material Handling Equipment Rentals
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- SEASONAL PRODUCTS
- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Demolition & Excavation
- Electrical & Mechanical
- Floor Protection
- Generators and Welders
- Construction Heaters
- Construction Ladders, Staging, & Storage
- Construction Lighting
- Man Lifts
- Material Handling Equipment
- Industrial Janitorial and Office Supplies
- Pressure Washers & Pumps
- Construction Safety Products
- Construction Safety Gear
- Surface Preparation
- Building Protection
- Diesel Accessories
- Zero Emissions
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rental
- Demolition & Excavation Equipment Rental
- General Construction Equipment Rental
- Generator Rentals and Welder Rentals
- Construction Heaters Rental
- Light Tower Rentals
- Man Lift Rentals
- Material Handling Equipment Rental
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- Concrete Floor Grinder Rentals
- Zero Emissions Rentals
- Repairs & Used
- Parts
- Blog
- Services
- Resources
- About Us
- Contact Us
Sales & Rental of Construction | Industrial Equipment & Supplies

2026 Top EVA Shoe Mould Types for Global Buyers?
The 2026 EVA Shoe Mould market is becoming more specialized, driven by lightweight footwear, sports recovery products, and fast regional production. Grand View Research and Fortune Business Insights both identify footwear as a major application area for EVA materials, supported by demand for cushioning, flexibility, and lower shoe weight. However, material growth does not automatically guarantee better mould performance.
Global buyers must compare mould types against production volume, foam expansion, product geometry, and factory equipment. Compression moulds remain practical for slippers, sandals, and selected casual soles. Injection moulds support higher repeatability and complex athletic footwear designs. Dual-density and multi-color moulds can combine visual appeal with different cushioning zones. Some factories also use specialized Phylon moulds for lightweight midsoles, although process control can become demanding.
World Footwear’s annual industry reports show the continued scale and geographic diversity of global footwear manufacturing. Production may shift between Asia, Europe, Latin America, and emerging markets. Therefore, an EVA Shoe Mould should be evaluated beyond its purchase price. Steel selection, cavity balance, venting, cooling, surface texture, and replacement-part access affect long-term cost.
Small details matter.
A 0.3-millimeter mismatch can create trimming problems. Uneven vents may leave visible marks on a white midsole. These examples are practical, but not universal. Factory skill still changes the result. Buyers should request trial samples, dimensional records, foam-density data, and documented quality procedures before approving a supplier. This guide examines the leading EVA Shoe Mould types for 2026, while recognizing one uncomfortable fact: no mould design fits every material, machine, or market.
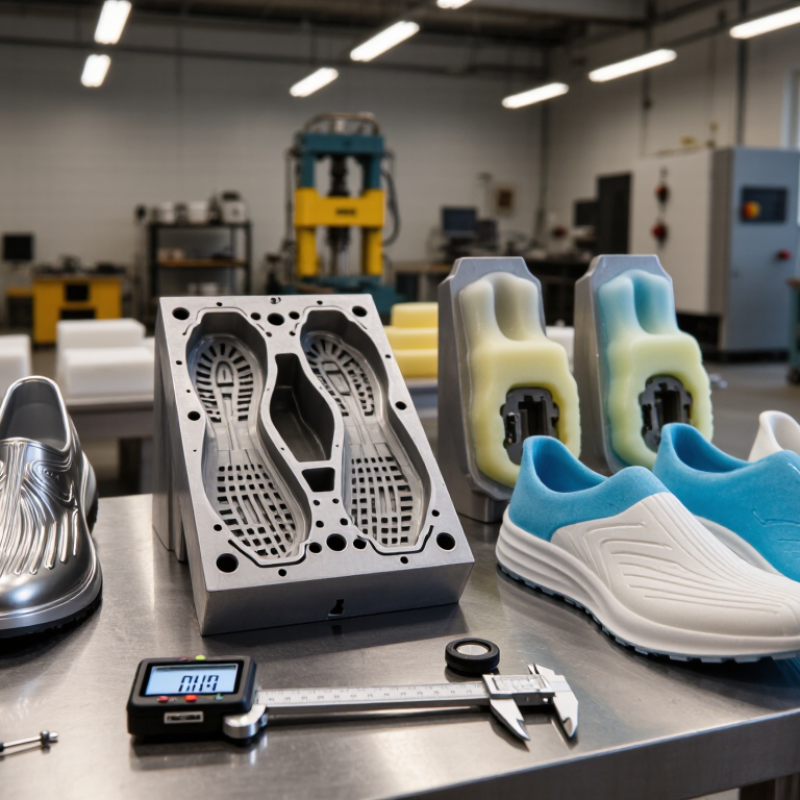
Table of Contents [Hide]
EVA Shoe Mould Basics and Manufacturing Principles
2026 Top EVA Shoe Mould Types for Global Buyers
EVA shoe moulds shape foam through heat, pressure, and controlled expansion. The main types are compression moulds and injection moulds. Compression moulding uses a measured EVA preform inside a heated cavity. Pressure then forces the material into the outsole pattern. Injection moulding feeds heated EVA directly into the cavity, supporting faster repeat production. The choice depends on volume, density, surface detail, and equipment capability.
World Footwear Yearbook 2023 recorded 23.9 billion pairs produced globally in 2022. Asia accounted for about 87.4% of that output. These figures explain the demand for stable mould cycles and consistent sizing. EVA pellets normally contain a foaming agent, crosslinking agent, and color additives. Heat activates the formulation. The material expands, bonds, and cools inside the mould. Small errors matter.
Cavity temperature, vent placement, and shrinkage allowance need practical testing. Aluminum moulds transfer heat quickly and suit many production runs. Steel inserts can improve wear resistance around sharp textures. A polished cavity may create a clean surface, while a textured cavity improves visual depth. Buyers should request trial data, not only drawings. A mould can look precise and still produce uneven density. That weakness is easy to miss. Measurements should include weight, hardness, expansion ratio, dimensional tolerance, and bonding performance. Test results sometimes disagree, so production conditions must be recorded honestly.
© Copyright - Pro Tool & Supply - Site by SVM E-Marketing Solutions - Sitemap
- Privacy policy