- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Concrete and Masonry
- Demolition & Excavation
- Electrical & Mechanical
- Fasteners and Anchoring Adhesives
- Floor Protection
- Generators and Welders
- Hand Tools
- Heaters
- Janitorial and Office Supplies
- Jobsite Protection
- Ladders & Storage
- Lighting & Lighting Accessories
- Man Lifts
- Material Handling Equipment
- Power Tools
- Pressure Washers & Pumps
- Safety Gear
- Safety Products
- Saws
- Surface Preparation
- SEASONAL PRODUCTS
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rentals
- Demolition & Excavation Equipment Rentals
- Concrete Floor Grinder Rentals
- General Construction Equipment Rentals
- Generator Rentals and Welder Rentals
- Heater Rentals
- Light Tower Rentals
- Man Lift Rentals in Massachusetts and Rhode Island
- Material Handling Equipment Rentals
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- SEASONAL PRODUCTS
- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Demolition & Excavation
- Electrical & Mechanical
- Floor Protection
- Generators and Welders
- Construction Heaters
- Construction Ladders, Staging, & Storage
- Construction Lighting
- Man Lifts
- Material Handling Equipment
- Industrial Janitorial and Office Supplies
- Pressure Washers & Pumps
- Construction Safety Products
- Construction Safety Gear
- Surface Preparation
- Building Protection
- Diesel Accessories
- Zero Emissions
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rental
- Demolition & Excavation Equipment Rental
- General Construction Equipment Rental
- Generator Rentals and Welder Rentals
- Construction Heaters Rental
- Light Tower Rentals
- Man Lift Rentals
- Material Handling Equipment Rental
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- Concrete Floor Grinder Rentals
- Zero Emissions Rentals
- Repairs & Used
- Parts
- Blog
- Services
- Resources
- About Us
- Contact Us
Sales & Rental of Construction | Industrial Equipment & Supplies

2026 Top Pasta And Noodle Maker Types for Global Buyers
The 2026 global pasta equipment market will demand more than attractive machinery. Buyers will seek dependable output, flexible formats, safer operation, and measurable operating costs. A modern Pasta And Noodle Maker may produce spaghetti, ramen, udon, macaroni, or filled pasta. Each format requires different pressure, cutting systems, dies, and moisture control.
Chef and pasta educator Evan Funke describes pasta as “a language.” This idea matters to equipment buyers. Machines must translate local recipes into consistent commercial results. A small restaurant may need a compact sheeter with quick cleaning. A factory may require continuous extrusion, automatic cutting, drying control, and digital monitoring. The correct choice depends on product goals, labor skills, production volume, and available space.
This guide examines the leading Pasta And Noodle Maker types for 2026. It compares countertop, semi-automatic, fully automatic, extrusion, sheeting, cutting, and multifunction models. It also considers stainless-steel construction, food-contact safety, energy use, voltage compatibility, spare parts, and after-sales support. These details can decide whether a machine becomes a reliable asset or an expensive interruption.
No machine is perfect. Even advanced systems need trained operators and regular maintenance. A glossy specification sheet can hide practical weaknesses. Cleaning time may be underestimated. Local service may also be limited. Global buyers should test dough performance, inspect finished samples, and request transparent warranty terms before purchase. The strongest decision combines technical evidence, hands-on experience, and realistic expectations.
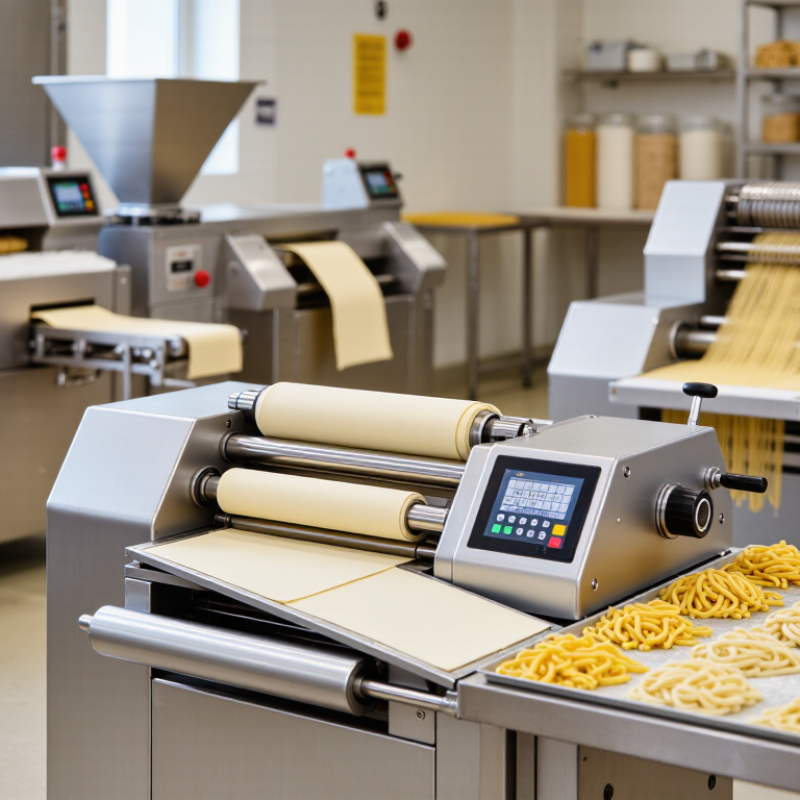
Table of Contents [Hide]
Pasta and Noodle Maker Types: Definitions and Main Categories
2026 Top Pasta and Noodle Maker Types for Global Buyers
Pasta and noodle makers are machines that mix, shape, cut, or process dough into consistent products. Their designs differ according to ingredients, production volume, and final shape. A small shop may need a countertop roller and cutter. A factory usually requires continuous feeding, extrusion, drying, or cooling equipment. The machine is not the product itself. It is one part of a controlled production line.
The main category is the roller-and-cutter maker. It presses dough into sheets, then cuts strips for products such as flat noodles or lasagna. Extrusion machines push dough through shaped dies. They can produce tubes, spirals, shells, and many other forms.
Fresh noodle machines often combine mixing, sheeting, cutting, and portioning in one frame. Hybrid systems offer flexible output, but their adjustments can be less intuitive. No category is perfect.
Buyers should check dough hydration, flour type, die material, cutting accuracy, and cleaning access. For example, a machine handling firm dough may need stronger drive components and wider feed openings. A restaurant may value quick changeovers more than maximum hourly output. A large processor may prioritize automation, safety guarding, spare parts, and stable temperature control. Capacity figures also need careful reading. They may describe ideal dough, not everyday production. Operators sometimes discover this difference after installation. That detail deserves more attention.
© Copyright - Pro Tool & Supply - Site by SVM E-Marketing Solutions - Sitemap
- Privacy policy